Labelling on automated lines
On an automated line nobody presses print.
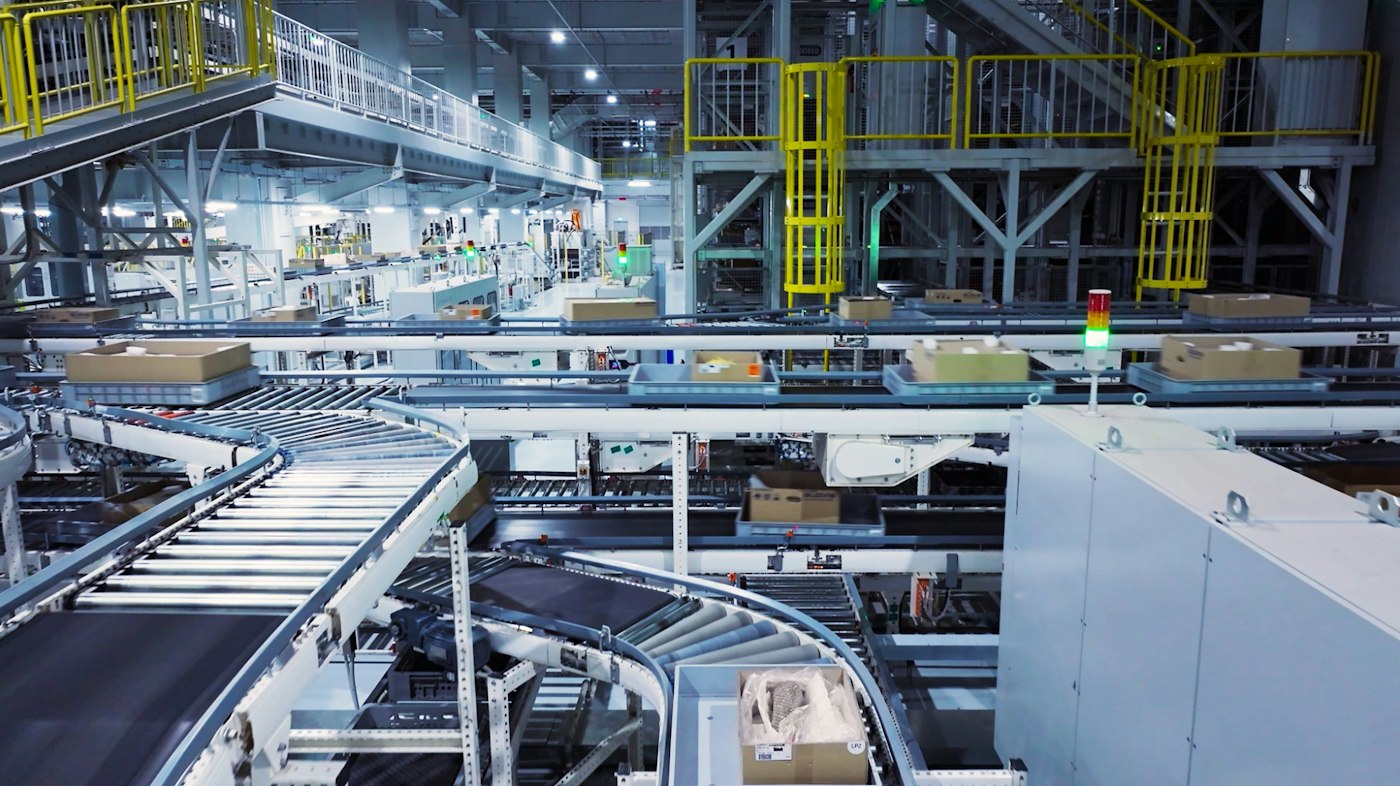
A product reaches the labelling station, the line controller says so, and a label has to be printed with the right data, applied in the right place and checked, in the time the line allows. When any of that fails, the line stops or, worse, a wrong label leaves the plant.
We build that part of the line: the label, the printer and the software between your ERP and your line controller.
What we connect
Your line controller. The PLC tells the label system that a product has arrived, which order it belongs to and when to print. We work with Siemens, Beckhoff and Rockwell controllers, over OPC UA or a digital I/O signal.
Your ERP. The order, batch and product data comes from SAP or your other ERP, so the label carries what the order says.
Print engines and applicators. Print engines built into the line, and print and apply systems that put the label on the product or the box. We install Zebra print engines, cab print and apply systems, and other leading brands.
Checks before the product moves on. A scanner reads the printed code, and a label that does not read, or reads the wrong data, stops the product.
An example line
To show how the parts fit, here is a typical set-up, described as an example rather than as a particular customer's line:
Drawn as an example. The carton labels carry a real GS1-128 with GS1's example company prefix 0614141.
| Line | Cartons of a finished product leave the packing machine, one every 2 seconds |
| Trigger | A Siemens PLC reports each carton and its order number over OPC UA |
| Data | SAP sends the order, batch and expiry date to TEKLYNX SENTINEL when the order starts |
| Print and apply | A cab print and apply system prints a GS1-128 carton label and applies it to the side of the carton |
| Check | A fixed scanner reads the label; a carton whose code does not read, or carries another batch, is pushed off the line |
| Record | Every printed and every rejected label is logged with time, order and batch |
What we write
Where the standard tools do not reach, we write the software: PLC programming for the labelling station, operator screens for the line, and the code that joins the line to the label software. Every line is different, so this is quoted per project after the free first review.
What stays with you
- The line itself, its safety and its mechanical integration, unless agreed otherwise.
- The rules for what happens when a label fails: reject, stop the line or alarm.
- In a GMP plant, the validation of the line, with our support as described in 1.3 Project responsibilities.
Preparing a validation, an inspection or a change to your labels?
The first engagement is free: a half-day review of your current label print chain, ending in a written list of gaps.